Use our free Drill Point Calculator to calculate drill tip length, point depth allowance, and the total tip depth needed to achieve a specified full-diameter hole depth. Simply enter your drill bit diameter, included point angle (such as 118° or 135°), and required hole depth to get instant results in metric or imperial units.
Not sure where to find your drill diameter, how to identify the correct point angle, or what hole depth to enter? We’ve included a complete step-by-step guide below the calculator explaining every input, calculation formula, depth measurement, and practical example to help you get accurate results.
Drill Point Calculator
Find the ideal conical drill-tip length and extra travel for a specified full-diameter hole depth.
Loading calculator… If it does not appear, please enable JavaScript.
How the calculation works
Formula: Point length = (drill diameter ÷ 2) ÷ tan(included point angle ÷ 2). Tip depth to achieve the specified full-diameter depth = full-diameter depth + point length.
Important: The calculation assumes a symmetric, ideal cone; split-point and reground drill tips may differ. It does not include breakthrough clearance or tool offsets.
What Is a Drill Point Calculator?
A Drill Point Calculator is an online tool that calculates the theoretical length of a drill bit’s pointed tip and determines how much additional drilling depth is needed to achieve a specified full-diameter hole.
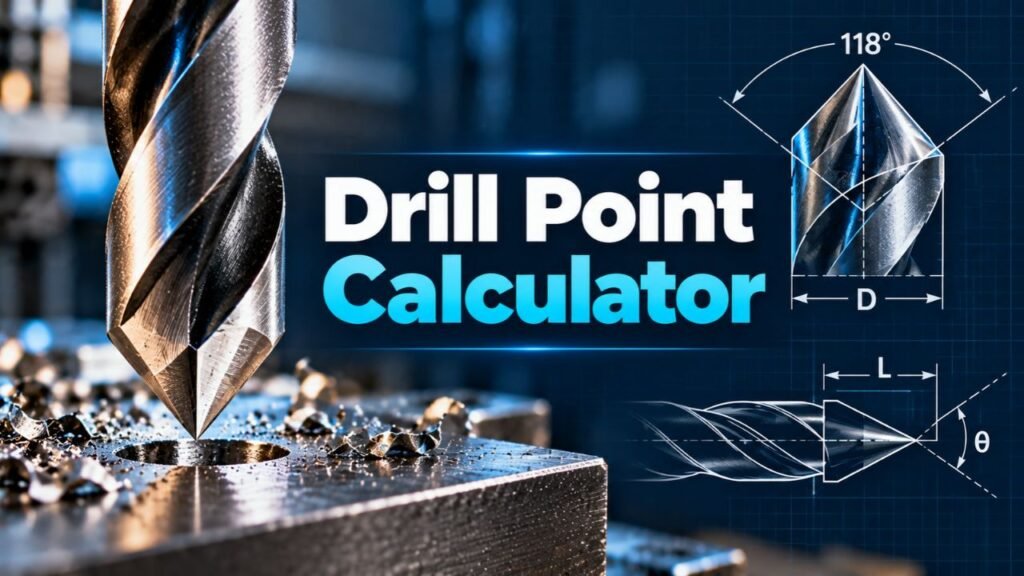
When you drill a hole using a conventional twist drill, the bottom of the hole is not flat. The drill’s pointed cutting geometry creates a cone-shaped bottom.
This means the drill tip extends beyond the point where the hole reaches its full diameter.
For many drilling applications, especially CNC machining and precision blind-hole drilling, understanding this additional depth is important.
Our free calculator helps you determine:
- Drill Point Length: The theoretical axial length of the drill’s conical tip.
- Required Tip Depth: The distance the drill tip must reach to achieve the specified full-diameter hole depth.
- Specified Full-Diameter Depth: The cylindrical hole depth entered into the calculator.
- Point-Length-to-Diameter Ratio: The relationship between drill diameter and point length.
The calculator supports metric and imperial measurements, including common drill point angles such as 118°, 135°, and custom included angles.
Whether you’re operating a drill press, CNC machining center, or another compatible drilling machine, the calculator can help you understand the geometry involved in hole-depth planning.
However, it calculates an ideal symmetrical conical point. Actual drill geometry can differ because of split points, web thinning, specialized cutting edges, tool wear, and regrinding.
This guide explains how to use every calculator input, identify your drill point angle, calculate drill tip length, and interpret drilling depths correctly.
How to Use the Drill Point Calculator
Our calculator requires three inputs:
- Drill bit diameter.
- Included point angle.
- Required full-diameter hole depth.
Follow these steps to calculate drill point length and theoretical tip depth.
Step 1: Select Metric or Imperial Units
First, choose the measurement system that matches your drilling project.
You can use:
Metric: Millimeters (mm).
Imperial: Inches (in).
For example, if your drill bit has a diameter of 10 mm, select metric.
If you’re using a 1/4-inch drill bit, select imperial and enter 0.25.
The calculator uses the selected measurement system for both diameter and depth.
Make sure the values you enter use the same measurement system.
Step 2: Enter the Drill Bit Diameter
Find the field labeled Drill Bit Diameter.
Enter the actual or nominal cutting diameter of your drill bit.
For example:
- 6 mm drill bit: Enter 6 in metric mode.
- 10 mm drill bit: Enter 10 in metric mode.
- 1/4-inch drill bit: Enter 0.25 in imperial mode.
- 3/8-inch drill bit: Enter 0.375 in imperial mode.
Use the drill’s cutting diameter rather than automatically entering its shank diameter or the drill chuck’s capacity.
If you don’t know the diameter, check the drill bit packaging, identification marking, manufacturer’s specification, or a suitable drill size gauge.
A detailed explanation of how to find and measure drill diameter is provided below.
Step 3: Enter the Included Drill Point Angle
Next, find the Included Point Angle field.
This is the angle formed by the two sides of the drill point when viewed in an axial section.
Common examples include:
- 118°
- 120°
- 135°
- 140°
For example, if your drill bit has a 118-degree point, enter:
118
If it has a 135-degree point, enter:
135
The calculator accepts the full included angle, not half the angle.
Do not enter 59° for a 118° drill simply because each side of the ideal cone makes a 59° angle with the drill axis.
Step 4: Enter the Required Full-Diameter Depth
The third field is Required Full-Diameter Depth.
This describes how deep you want the hole to extend at its full nominal diameter, excluding the pointed bottom.
For example, suppose your machining drawing specifies a 10 mm diameter hole with 20 mm of full-diameter depth.
Enter:
Required Full-Diameter Depth = 20 mm
The calculator will add the theoretical drill point length to determine the total tip depth.
Important: If your drawing specifies the depth to the drill tip rather than the full-diameter portion, do not enter that value as full-diameter depth without converting it.
The distinction is explained later in this guide.
Step 5: Review the Calculated Results
After entering the values, the calculator displays the theoretical results.
For example, using:
| Input | Value |
|---|---|
| Drill diameter | 10 mm |
| Included point angle | 118° |
| Full-diameter hole depth | 20 mm |
The calculator returns approximately:
| Result | Value |
|---|---|
| Drill point length | 3.0043 mm |
| Required tip depth | 23.0043 mm |
| Full-diameter depth | 20 mm |
| Point-length / diameter ratio | 0.30043 |
This means the theoretical drill tip needs to reach approximately 23.0043 mm below the entry surface to create 20 mm of full-diameter hole.
The extra 3.0043 mm represents the ideal conical drill point.
Step 6: Calculate Drill Point Length Without a Hole Depth
You can also calculate the drill point length by itself.
To do this:
- Enter the drill diameter.
- Enter the included point angle.
- Set Required Full-Diameter Depth to 0.
The calculator will display the theoretical drill point length.
This is useful when you only want to know the tip length or compare different point angles.
Understanding the Parts of a Twist Drill
Before calculating drill point geometry, it helps to understand the main parts of a conventional twist drill.
Drill Diameter
The drill diameter is the nominal size of the hole the tool is designed to produce.
It is measured across the cutting diameter near the outer cutting corners.
For a conventional 10 mm twist drill, the nominal diameter is 10 mm.
Drill Point
The drill point is the cutting end of the twist drill.
Its geometry influences how the drill begins cutting and enters the workpiece.
Cutting Lips
The cutting lips are the primary cutting edges of the drill point.
A conventional twist drill typically has two principal cutting lips.
Chisel Edge
The chisel edge is located near the center of a conventional drill point.
Its shape and length depend on the drill’s geometry.
Some specialized drills use split-point or thinned-web designs that change the center geometry.
Flutes
The flutes are the helical grooves running along the drill body.
They help form cutting edges and provide passages for chips to leave the hole.
Shank
The shank is the portion held by the drill chuck, collet, or other compatible toolholding system.
Its diameter may be the same as or different from the cutting diameter.
Drill Point Angle
The drill point angle describes the included angle of the drill tip.
It is one of the two principal inputs used to calculate theoretical drill point length.
Drill Point Length
Drill point length is the axial distance from the theoretical apex of the cone to the plane where the cone reaches the drill’s full diameter.
It is not the same as the drill’s overall length, flute length, or cutting depth.
Where to Find Your Drill Bit Diameter
Finding the correct drill diameter is usually straightforward, but there are a few details worth checking.
1. Check the Drill Bit Packaging
Many drill bits are sold in packaging that identifies their nominal size.
For example:
10 mm HSS Twist Drill
This indicates a nominal cutting diameter of 10 mm.
Another package might say:
1/4-Inch Cobalt Drill Bit
This indicates a nominal diameter of 0.25 inch, equivalent to 6.35 mm.
Use this nominal cutting diameter in the calculator unless manufacturer instructions specify a different effective dimension for the operation.
2. Look for Markings on the Drill Shank
Some drill manufacturers mark the diameter on the shank.
You might see markings such as:
- 6.0
- 8.0
- 10.0
- 1/4
- 3/8
The marking format depends on the manufacturer.
If the drill has only a product number, search the manufacturer’s catalog for its specifications.
3. Check the Manufacturer’s Product Specifications
Manufacturer product pages often list:
- Nominal drill diameter.
- Cutting diameter tolerance.
- Shank diameter.
- Drill point angle.
- Flute length.
- Overall length.
- Tool material.
- Coating.
For a basic twist-drill point calculation, use the appropriate cutting diameter.
4. Measure With a Suitable Measuring Tool
If the drill size is unknown, you may be able to measure it with a suitable micrometer or caliper.
For a conventional twist drill, the cutting diameter is associated with the outer margins near the drill point.
Use care when measuring the cutting end, as sharp edges and flute geometry can make measurements difficult.
Only handle or measure a drill when it is safely removed from service or the machine is stopped and isolated according to its operating instructions.
5. Use a Drill Bit Size Gauge
A drill gauge contains accurately sized holes or other reference features for identifying common drill sizes.
This can help identify an unmarked drill bit.
Make sure the gauge matches the sizing system you are using.
Common Drill Bit Size Conversion Chart
| Fractional size | Decimal inches | Millimeters |
|---|---|---|
| 1/16 inch | 0.0625 | 1.5875 |
| 1/8 inch | 0.1250 | 3.1750 |
| 3/16 inch | 0.1875 | 4.7625 |
| 1/4 inch | 0.2500 | 6.3500 |
| 5/16 inch | 0.3125 | 7.9375 |
| 3/8 inch | 0.3750 | 9.5250 |
| 7/16 inch | 0.4375 | 11.1125 |
| 1/2 inch | 0.5000 | 12.7000 |
You can convert inches into millimeters using:
Millimeters = Inches × 25.4
To convert millimeters into inches:
Inches = Millimeters ÷ 25.4
What About Number and Letter Drill Bits?
US drill sets may include numbered or letter-sized drill bits.
For example, a #7 drill has a nominal diameter of 0.2010 inch.
This is approximately 5.1054 mm.
When using a numbered or letter drill, consult a drill bit size chart to find the corresponding decimal diameter.
Enter that decimal measurement into the calculator.
Where to Find the Drill Point Angle
The point angle is just as important as diameter.
Entering the wrong angle can produce an incorrect tip length and hole-depth allowance.
1. Check the Drill Bit Packaging
Many manufacturers identify the included point angle on the packaging.
You may see descriptions such as:
- 118° Point.
- 135° Split Point.
- 140° Point.
If your drill packaging clearly identifies the point angle, use that value.
However, avoid assuming a point angle from the drill material alone.
For example, not every cobalt drill has the same point angle.
2. Check the Manufacturer’s Product Page
A manufacturer’s technical specification is often the most reliable source.
Look for:
Point Angle, Drill Point Angle, or Included Angle.
If you have the drill’s model or part number, use it to locate the exact specification.
3. Use a Drill Point Gauge
A drill point gauge is designed to inspect drill point angles and, on some models, cutting lip geometry.
A typical gauge may have reference angles such as 118° or 135°.
It can help determine whether a conventional twist drill matches the intended point angle.
For precise inspection, use appropriate measuring equipment and the manufacturer’s inspection procedure.
4. Check After Resharpening
A drill that has been manually resharpened may no longer have its original point angle.
For example, a drill originally manufactured with a 118° point could have a different geometry after regrinding.
If the actual point angle matters for a tight depth tolerance, measure the resharpened tool rather than relying only on its original packaging.
5. Don’t Confuse Point Angle With Other Drill Angles
A twist drill has several different geometric angles.
| Angle | Meaning |
|---|---|
| Point angle | Included angle at the drill tip |
| Helix angle | Angle of the spiral flutes |
| Lip relief angle | Clearance behind the cutting edge |
| Chisel edge angle | Geometry associated with the center chisel edge |
Our calculator requires the included point angle.
It does not require the helix angle, lip relief angle, or chisel edge angle.
Drill Point Length Calculation Formula
The drill point length formula comes from the geometry of a right triangle formed by an ideal conical drill tip.
Main Drill Point Length Formula
Drill Point Length = (Drill Diameter ÷ 2) ÷ tan(Point Angle ÷ 2)
Mathematically:
L = D / [2 × tan(θ / 2)]
Where:
- L = theoretical drill point length.
- D = drill cutting diameter.
- θ = included point angle.
- tan = trigonometric tangent function.
The diameter and calculated length use the same unit system.
For example, if the diameter is entered in millimeters, the resulting point length is in millimeters.
If diameter is entered in inches, the result is in inches.
Why Is the Point Angle Divided by Two?
A conventional symmetric drill point can be approximated as a cone.
When the cone is divided along its centerline, each half forms a right triangle.
The radius of the drill is one side of the triangle.
The axial point length is another side.
The angle between the drill axis and the ideal cone surface is half the full included point angle.
Therefore:
tan(θ / 2) = (D / 2) ÷ L
Rearranging this equation gives the drill point length formula.
Does the Formula Work for Inches and Millimeters?
Yes.
The formula is dimensionally consistent.
You do not need different geometric equations for metric and imperial measurements.
Just make sure the diameter and depth use the same unit system.
Important Geometry Assumption
The equation assumes a symmetric conical point with a well-defined apex and full cutting diameter.
Many real drill points are not perfect cones.
Split-point drills, web-thinned drills, reground cutters, and specialized designs can have different actual tip profiles.
For critical dimensions, the manufacturer’s tool geometry or a verified measurement takes priority over the ideal cone model.
How to Calculate Drill Point Depth Allowance
Drill point depth allowance is the additional axial distance associated with the pointed end of a conventional twist drill.
For an ideal cone, it is equal to the theoretical point length.
Therefore:
Point Depth Allowance = Drill Point Length
If the machining drawing specifies a full-diameter hole depth, the corresponding theoretical tip depth is:
Required Tip Depth = Full-Diameter Hole Depth + Drill Point Length
Or:
Htip = Hfull + L
Where:
- Htip = theoretical depth reached by the drill tip.
- Hfull = required cylindrical hole depth at full diameter.
- L = drill point length.
This distinction is especially important for blind-hole drilling.
118° Drill Point Length Formula
A 118-degree point is common on general-purpose twist drills.
For a 118° point:
L = D / [2 × tan(59°)]
The resulting factor is approximately:
L ≈ 0.30043 × D
For quick workshop estimates, this is often rounded to:
Point Length ≈ Drill Diameter × 0.30
Example: 10 mm Drill With a 118° Point
Drill diameter = 10 mm.
Point angle = 118°.
L = 10 ÷ [2 × tan(59°)]
Drill Point Length ≈ 3.0043 mm
This means the ideal conical point extends approximately 3 mm beyond the full-diameter cutting corners.
If you require a 20 mm full-diameter blind hole:
Required Tip Depth = 20 + 3.0043
Required Tip Depth ≈ 23.0043 mm
135° Drill Point Length Formula
A 135-degree point is another common drill geometry.
For a 135° included angle:
L = D / [2 × tan(67.5°)]
This gives:
L ≈ 0.20711 × D
For quick calculations:
Point Length ≈ Drill Diameter × 0.207
Example: 10 mm Drill With a 135° Point
Drill diameter = 10 mm.
Point angle = 135°.
L = 10 ÷ [2 × tan(67.5°)]
Drill Point Length ≈ 2.0711 mm
If the required full-diameter depth is 20 mm:
Required Tip Depth = 20 + 2.0711
Required Tip Depth ≈ 22.0711 mm
Notice that the 135° point requires less additional depth than the 118° point for the same diameter.
118° vs. 135° Drill Point: What’s the Difference?
These two angles are among the most commonly encountered drill point geometries.
| Feature | 118° Point | 135° Point |
|---|---|---|
| Included angle | 118° | 135° |
| Ideal tip geometry | Longer cone | Shorter, flatter cone |
| Point length factor | 0.30043 × D | 0.20711 × D |
| Tip length for 10 mm diameter | 3.0043 mm | 2.0711 mm |
| Full-depth allowance | Greater | Smaller |
| Common configurations | General-purpose twist drills | Frequently used with split-point designs |
A larger included point angle creates a shorter theoretical conical point.
This means the full drill diameter is reached with less axial travel beyond the tip.
However, point angle alone does not determine which drill bit is best for a particular material.
Drill construction, cutting-edge design, coatings, and manufacturer recommendations also matter.
Does a 135° Drill Always Have a Split Point?
No.
Point angle and split-point geometry describe different features.
A drill may have a 135° included angle and a split-point design, but those characteristics are not interchangeable.
If the drill has a split point or other modified center geometry, its actual tip length may differ from the ideal conical calculation.
Which Angle Should You Enter?
Enter the actual included point angle specified for your drill.
Do not choose 118° or 135° simply because one produces a more convenient depth.
The calculator is intended to describe the drill geometry you have, not select a drill point angle automatically.
Drill Point Length Factor Chart
The following table shows theoretical point-length factors for common included angles.
| Included angle | Point length factor | Length for 10 mm drill |
|---|---|---|
| 90° | 0.50000 × D | 5.0000 mm |
| 100° | 0.41955 × D | 4.1955 mm |
| 118° | 0.30043 × D | 3.0043 mm |
| 120° | 0.28868 × D | 2.8868 mm |
| 130° | 0.23315 × D | 2.3315 mm |
| 135° | 0.20711 × D | 2.0711 mm |
| 140° | 0.18199 × D | 1.8199 mm |
These factors represent ideal geometric cones.
They are not material-specific drilling recommendations.
Drill Point Length Chart for Common Sizes
Here is a quick metric reference for 118° and 135° included point angles.
| Drill diameter | 118° point length | 135° point length |
|---|---|---|
| 5 mm | 1.5022 mm | 1.0355 mm |
| 6 mm | 1.8026 mm | 1.2426 mm |
| 8 mm | 2.4034 mm | 1.6569 mm |
| 10 mm | 3.0043 mm | 2.0711 mm |
| 12 mm | 3.6052 mm | 2.4853 mm |
| 16 mm | 4.8069 mm | 3.3137 mm |
| 20 mm | 6.0086 mm | 4.1421 mm |
Imperial Drill Point Length Chart
| Drill diameter | 118° point length | 135° point length |
|---|---|---|
| 1/8 inch | 0.03755 in | 0.02589 in |
| 1/4 inch | 0.07511 in | 0.05178 in |
| 3/8 inch | 0.11266 in | 0.07767 in |
| 1/2 inch | 0.15022 in | 0.10355 in |
For custom point angles or drill sizes, use the calculator above instead of relying on rounded chart values.
Drill Point Calculator Examples
The following examples demonstrate how drill point length and tip depth are calculated.
These values are theoretical geometry calculations. They do not include tool offsets, breakthrough clearance, additional machining allowances, or actual tool-point deviations.
Example 1: 118° Drill, 10 mm Diameter, 20 mm Hole
Inputs:
| Parameter | Value |
|---|---|
| Drill diameter | 10 mm |
| Point angle | 118° |
| Required full-diameter depth | 20 mm |
First calculate the point length:
L = 10 ÷ [2 × tan(59°)]
L ≈ 3.0043 mm
Now calculate the required tip depth:
Htip = 20 + 3.0043
Required Tip Depth = 23.0043 mm
If the depth reference is the workpiece entry surface, the theoretical tip reaches 23.0043 mm below that surface when the full-diameter section reaches 20 mm.
Example 2: 135° Drill, 12 mm Diameter, 25 mm Hole
Inputs:
| Parameter | Value |
|---|---|
| Drill diameter | 12 mm |
| Point angle | 135° |
| Required full-diameter depth | 25 mm |
Point length:
L = 12 ÷ [2 × tan(67.5°)]
L ≈ 2.4853 mm
Required tip depth:
Htip = 25 + 2.4853
Required Tip Depth ≈ 27.4853 mm
The additional 2.4853 mm represents the theoretical conical drill point.
Example 3: 1/4-Inch Drill With a 118° Point
Suppose you’re using a 1/4-inch twist drill.
Inputs:
- Drill diameter: 0.250 inch.
- Point angle: 118°.
- Required full-diameter hole depth: 0.750 inch.
Calculate point length:
L = 0.250 ÷ [2 × tan(59°)]
L ≈ 0.07511 inch
Calculate total tip depth:
Htip = 0.750 + 0.07511
Required Tip Depth ≈ 0.82511 inch
This is the theoretical depth to the drill tip.
Example 4: Compare 118° and 135° Drill Points
Suppose you use two drill bits of the same diameter:
Drill Diameter = 10 mm
The first has a 118° point.
The second has a 135° point.
| Point angle | Theoretical point length |
|---|---|
| 118° | 3.0043 mm |
| 135° | 2.0711 mm |
Difference:
3.0043 − 2.0711 = 0.9332 mm
The 118° drill has approximately 0.93 mm more theoretical point length.
This difference matters when calculating deep blind holes, shallow holes, or the material remaining below the drill tip.
What Is the Difference Between Drill Point Depth and Hole Depth?
This is one of the most important concepts in drilling geometry.
A conventional twist drill produces a hole with a conical bottom.
That means there are two different depth measurements.
1. Full-Diameter Hole Depth
Full-diameter depth measures how far the cylindrical portion of the hole extends.
For example, a drawing may require:
Ø10 mm × 20 mm Full-Diameter Depth
This means the hole must maintain its full 10 mm nominal diameter for 20 mm below the specified reference surface.
The pointed bottom extends beyond that depth.
2. Drill Tip Depth
Tip depth measures the deepest point reached by the drill’s theoretical tip.
For a conventional pointed drill, this is deeper than the full-diameter portion.
For example:
- Full-diameter depth: 20 mm.
- Drill point length: 3 mm.
- Theoretical tip depth: 23 mm.
Why This Difference Matters
Suppose you stop the tip of a 10 mm, 118° drill exactly 20 mm below the entry surface.
The full-diameter portion will not extend to 20 mm.
Its theoretical full-diameter depth would be:
20 − 3.0043
Approximately 16.9957 mm
This is shorter than the intended 20 mm cylindrical depth.
On a precision machining drawing, that difference may be unacceptable.
What If the Drawing Specifies Tip Depth?
If the drawing specifically gives the depth to the drill tip, do not add the point allowance again.
Instead, if needed, calculate the full-diameter depth using:
Full-Diameter Depth = Tip Depth − Drill Point Length
This assumes the tip has traveled far enough for the drill to create a full-diameter cylindrical section.
Always confirm the drawing’s dimensioning convention.
Drill Point Allowance for Blind Holes
A blind hole does not extend completely through the workpiece.
Its bottom usually includes the conical profile left by the drill point.
For a blind hole, you may need to consider both the required full-diameter depth and the remaining material beneath the drill tip.
Calculating Remaining Material Thickness
If you know the material thickness and theoretical drill tip depth:
Remaining Thickness = Material Thickness − Drill Tip Depth
For example:
- Material thickness: 25 mm.
- Drill diameter: 10 mm.
- Point angle: 118°.
- Full-diameter depth: 20 mm.
Point length:
3.0043 mm
Tip depth:
23.0043 mm
Remaining thickness:
25 − 23.0043
Remaining Thickness ≈ 1.9957 mm
This is the theoretical amount of material remaining beneath the drill tip.
The calculation does not establish whether that remaining thickness is structurally adequate or safe for the intended application.
Why You Should Check the Remaining Thickness
If the drill point gets too close to the opposite surface, you may risk unintended breakthrough or violating the specified minimum wall thickness.
Factors such as material tolerances, tool geometry, deflection, runout, and setup errors can affect the actual result.
For critical holes, verify the required remaining material thickness and drilling process with the engineering drawing and suitable inspection procedures.
How to Calculate Drill Point Allowance for Through Holes
A through hole extends completely through the material.
With a pointed drill, the tip reaches the far side before the hole is fully opened to its nominal diameter.
Example: Drilling Through an 8 mm Plate
Suppose you have:
- Material thickness: 8 mm.
- Drill diameter: 10 mm.
- Point angle: 118°.
The theoretical point length is:
L ≈ 3.0043 mm
To bring the full cutting diameter to the far surface, the theoretical tip depth from the entry surface is:
8 + 3.0043
Approximately 11.0043 mm
This is a geometrical minimum for the ideal point profile.
It does not include any additional clearance that might be necessary for your actual drilling setup.
Does the Drill Need Extra Breakthrough Clearance?
Depending on the operation, additional clearance may be required to account for tool geometry, part tolerances, machine setup, or complete breakthrough.
However, that allowance should not be chosen randomly.
Verify that sufficient clearance exists beneath the workpiece and that the drill cannot collide with the fixture, machine table, or other components.
Our calculator does not automatically add breakthrough clearance.
How to Use Drill Point Calculations for CNC Drilling
CNC drilling is one of the applications where point-length calculations can be particularly useful.
A machining drawing may specify a hole depth, but the CNC program must use a depth convention compatible with the controller, tooling offsets, and CAM setup.
Step 1: Read the Engineering Drawing
Determine whether the specified hole depth refers to:
- Full-diameter cylindrical depth.
- Depth to the theoretical drill tip.
- Another defined geometric feature.
Do not assume these values are interchangeable.
Step 2: Identify the Drill Geometry
Determine the actual drill diameter and point angle.
For example:
- Diameter: 10 mm.
- Included point angle: 118°.
Use the manufacturer’s specifications or appropriate tool inspection data.
Step 3: Calculate Point Allowance
Use the calculator to determine the additional conical point length.
For the example:
Point Allowance ≈ 3.0043 mm
Step 4: Determine the Required Tip Depth
If the drawing requires 20 mm of full-diameter depth:
20 + 3.0043 = 23.0043 mm.
This gives the ideal tip depth below the entry surface.
Step 5: Verify Your CNC Setup
Before using this result in a CNC program, confirm:
- Work coordinate and datum location.
- Tool length compensation.
- Whether the programmed depth refers to the drill tip or another tool reference.
- Controller and drilling-cycle behavior.
- Material thickness and fixture clearance.
- Tool geometry and machining tolerances.
- Required chip evacuation and drilling strategy.
Important: The calculator’s Required Tip Depth output is a geometric distance, not a ready-to-run CNC Z command.
In a common setup with the workpiece top at Z0 and the drill tip used as the tool reference, drilling below the surface may use a negative Z coordinate.
However, actual sign conventions, reference points, compensation, and cycle behavior depend on the specific CNC setup.
Never paste a calculated depth directly into a machine program without verifying those details.
Drill Point Angle vs. Spot Drill Angle
Drill point angle and spot drill angle are related but serve different functions.
A twist drill creates the primary hole.
A spot drill may create an initial locating feature to guide a subsequent drilling operation.
In some machining applications, an appropriately selected spotting angle can help the main drill enter more consistently.
However, spot drill angle selection depends on the main drill’s point geometry and manufacturer recommendations.
An incorrectly selected spotting geometry can create undesirable cutting-edge engagement.
Our Drill Point Calculator does not automatically determine the correct spotting-drill angle.
It calculates the axial length of a theoretical conical point.
For spot-drilling applications, consult the cutting-tool manufacturer’s technical recommendations.
Can You Use This Calculator for Split-Point Drills?
You can use the calculator to estimate a theoretical conical point length using the drill’s nominal included angle.
However, split-point drills often have modified center geometry.
The actual point may not match a perfect cone.
This means the calculated result may differ from the actual tool profile.
If you’re drilling a hole where the exact bottom geometry or depth tolerance matters, use the drill manufacturer’s technical drawing or an appropriate measurement.
Do not treat the ideal-cone output as a verified measurement of every split-point drill.
Can You Use It for Brad-Point, Step, or Flat-Bottom Drill Bits?
Not as a universal geometry model.
Our calculator is designed primarily for conventional symmetrical conical twist-drill points.
Other drill types may have different cutting geometry.
Brad-Point Drill Bits
Brad-point drills have a projecting center point and outer cutting spurs.
Their tip geometry does not match a simple cone.
The calculator cannot reliably determine the actual full-depth allowance for every brad-point design.
Step Drill Bits
Step drills have multiple cutting diameters and transitions.
Their geometry must be evaluated according to the particular step and cutting profile.
A single diameter and point angle cannot describe the entire tool.
Spade Bits
Spade bits generally have a different cutting arrangement, often including a projecting center point.
The ideal conical twist-drill formula is not an appropriate full description of their geometry.
Flat-Bottom Drills
Flat-bottom drills have substantially different end geometry.
A theoretical cone allowance is generally not appropriate for describing their bottom profile.
Countersink Cutters
Countersink geometry can involve a conical cutting surface, but the relevant depth depends on the starting hole diameter and final countersink diameter.
A conventional drill point calculation does not automatically provide countersink depth.
Use a dedicated countersink depth calculator for that application.
Does Drill Point Angle Affect Hole Accuracy?
Drill point geometry can affect drilling behavior.
Point angle, chisel edge design, cutting lip symmetry, cutting-edge sharpness, and drill rigidity all influence the way a drill enters the material.
However, point angle alone does not determine hole accuracy.
Other factors include:
- Tool runout.
- Drill wear.
- Workholding stability.
- Machine rigidity.
- Material characteristics.
- Feed rate and spindle speed.
- Cooling and chip evacuation.
- Spotting or pilot-hole strategy where appropriate.
Our calculator does not predict hole diameter tolerance, position accuracy, drill wandering, or surface finish.
It focuses on theoretical axial point geometry.
Common Drill Point Calculation Mistakes
1. Entering Half the Point Angle
If your drill is labeled 118°, enter 118.
Do not enter 59.
The calculator divides the included angle by two internally.
2. Confusing Hole Depth With Tip Depth
The full-diameter depth and tip depth are not the same for a conventional pointed drill.
Confirm which dimension your drawing requires.
3. Using Shank Diameter Instead of Cutting Diameter
Some drills have reduced shanks.
Use the appropriate nominal cutting diameter, not automatically the shank diameter.
4. Assuming All Drills Have 118° Points
Although 118° is common, many drills use other angles.
Always check the actual tool specifications.
5. Using the Ideal Formula for Unusual Tip Geometry
Split points, brad points, step drills, and specialized tools may not match a symmetric conical point.
6. Mixing Metric and Imperial Units
Make sure diameter and hole depth use the correct unit system.
For example, entering 0.25 in metric mode means 0.25 mm, not 1/4 inch.
7. Forgetting to Check the Remaining Material
A blind hole may leave less material beneath the drill tip than expected.
Evaluate the actual tip depth against the workpiece thickness.
8. Ignoring Tool Length Offsets
A geometric tip depth is not necessarily the same as a CNC controller’s programmed coordinate.
Verify the machine setup.
9. Adding Point Allowance Twice
If the specified depth already refers to the drill tip, adding the point length again would increase the intended tip depth unnecessarily.
10. Assuming the Formula Includes All Machining Allowances
The calculator does not automatically account for breakthrough clearance, tool wear, regrinding, toolholder offsets, or machine-specific process allowances.
Safety Tips for Drill Point and Hole Depth Calculations
Depth calculations are important, but safe drilling also requires proper equipment setup.
Before using calculated values:
- Confirm the drill diameter and actual point geometry.
- Verify the workpiece thickness and drilling location.
- Check whether the hole is blind or through.
- Confirm the required depth convention on the engineering drawing.
- Secure the workpiece appropriately.
- Check that the drill cannot contact the machine table or fixtures.
- Follow the machine’s operating and guarding instructions.
- Use appropriate eye protection and chip-removal procedures.
- Never measure or touch a rotating drill.
- Follow the tool manufacturer’s recommendations for speed, feed, and cooling.
- Verify CNC tool offsets, coordinates, and drilling cycles before machining.
If an operation involves a critical minimum wall thickness, tight tolerance, or safety-sensitive part, use approved engineering and inspection procedures rather than relying solely on a theoretical calculator.
Frequently Asked Questions
What is a drill point calculator?
A drill point calculator determines the theoretical axial length of a conical drill tip using drill diameter and included point angle.
It can also calculate the tip depth required to achieve a specified full-diameter hole depth.
How do you calculate drill point length?
Use:
Point Length = Drill Diameter ÷ [2 × tan(Point Angle ÷ 2)]
This formula assumes a symmetric conical point.
What is the drill point depth formula?
For a hole specified by its full-diameter depth:
Tip Depth = Full-Diameter Depth + Point Length
How do you calculate a 118-degree drill point?
Multiply the drill diameter by approximately 0.30043.
For example:
10 mm × 0.30043 ≈ 3.0043 mm.
How do you calculate a 135-degree drill point?
Multiply the drill diameter by approximately 0.20711.
For example:
10 mm × 0.20711 ≈ 2.0711 mm.
What is the point length of a 1/4-inch drill?
For a theoretical 118° point, the point length is approximately 0.07511 inch.
For a 135° point, it is approximately 0.05178 inch.
What is the point length of a 10 mm drill?
It depends on the included point angle.
A 10 mm drill with a 118° point has a theoretical point length of approximately 3.0043 mm.
At 135°, the theoretical length is approximately 2.0711 mm.
What is the difference between 118° and 135° drill points?
The 118° point is longer and more pointed.
The 135° point has a wider included angle and a shorter ideal conical length.
The appropriate drill geometry depends on the cutting-tool design and application.
Is 135° better than 118°?
Not universally.
The best choice depends on the workpiece material, drill construction, machine, and manufacturer’s recommendations.
A shorter theoretical point length alone does not determine which drill will perform better.
Does a larger point angle create a shorter tip?
Yes, for an ideal symmetric cone with the same drill diameter.
As the included angle increases, the theoretical axial point length decreases.
Does a larger drill diameter increase point length?
Yes, if the point angle remains constant.
The theoretical point length is directly proportional to diameter.
Doubling the diameter doubles the point length.
Where can I find the drill point angle?
Check the manufacturer specifications, original packaging, product documentation, or a suitable drill point gauge.
If the drill has been resharpened, its actual geometry should be verified.
Can I measure the drill point angle?
Yes, using an appropriate drill point gauge or other suitable precision inspection equipment.
Avoid assuming an angle based only on visual appearance.
Is drill point length the same as flute length?
No.
Point length is the axial length of the pointed tip.
Flute length is associated with the grooved portion of the drill body.
They describe different dimensions.
Is drill point depth the same as total drill length?
No.
Drill point depth refers to the axial point geometry or the depth reached by the tip.
Overall drill length includes the body, flutes, shank, and point.
Why do I need to add drill point allowance?
If the specified hole depth refers to the full-diameter cylindrical portion, the tip must travel farther to allow the full drill diameter to reach that depth.
Do I always add point allowance to blind-hole depth?
Only when the depth convention requires it.
If the specified depth already refers to the tip, adding the allowance again would be incorrect.
Always check the drawing.
Can I use this calculator for through holes?
You can use the calculated point length when determining theoretical full-diameter breakthrough depth.
However, additional clearances and machine setup requirements must be evaluated separately.
Can I use this calculator for CNC drilling?
Yes, for theoretical point geometry and hole-depth planning.
However, the output is not a complete CNC drilling-cycle command.
Does the calculator automatically provide CNC Z coordinates?
No.
It provides theoretical depth distances.
Actual CNC coordinates depend on work offsets, tool length compensation, controller behavior, and the machining setup.
Can I use the calculator for a handheld drill?
You can use it to understand conventional drill point geometry.
However, handheld drilling generally offers less precise control over axial depth than a properly configured machine-controlled process.
Can I use it for split-point drills?
It can provide a conical approximation, but split-point geometry may differ from the ideal model.
For precision applications, verify the actual tool profile.
Can I calculate drill point length for custom angles?
Yes.
Enter the required included point angle directly into the calculator.
The formula works for an ideal symmetric cone with a valid point angle.
What if I only need drill tip length?
Enter your drill diameter and point angle, then set the required full-diameter depth to zero.
The calculator will display the theoretical point length.
Does the calculator support inches and millimeters?
Yes.
You can select imperial or metric units for diameter and depth.
Does this calculator calculate drill speed or feed rate?
No.
Drill point length is a geometry calculation.
To calculate rotational speed and axial feed rate, use our separate Drill Speed and Feed Calculator.
Is this Drill Point Calculator free?
Yes.
The calculator can be used directly in your browser without downloading additional software or purchasing a subscription.
Final Thoughts
Our free Drill Point Calculator provides a straightforward way to calculate theoretical drill tip length, point depth allowance, and required tip depth using drill diameter and included point angle.
Understanding the difference between full-diameter hole depth and drill tip depth is especially useful when planning CNC drilling, blind holes, and other precision drilling operations.
For reliable results, remember these important principles:
Use the correct cutting diameter. Check the drill specifications rather than assuming the shank diameter is always the same.
Verify the point angle. Common values such as 118° and 135° produce different point lengths, but the correct input is the actual included angle of your drill.
Understand the hole depth convention. A dimension to the drill tip is different from a dimension requiring full-diameter cylindrical depth.
Account for actual drill geometry. Split points, modified cutting edges, regrinding, and other tool features can affect the real point profile.
Check the complete machining setup. Calculated tip depth does not automatically account for machine offsets, breakthrough clearance, tool deflection, or workpiece tolerances.
Whether you’re learning drilling geometry or preparing a machining operation, this calculator helps simplify the mathematical relationship between drill diameter, point angle, and hole depth.
Use the calculator above whenever you need a quick theoretical drill point calculation, and refer to this guide whenever you need help identifying an input or interpreting the results.